7 Rapid Injection Molding Tips for Global Buyers?
Global buyers are under pressure to launch molded parts faster, control costs, and reduce supply-chain surprises. Rapid Injection Molding can shorten the path from a validated design to production parts, but speed alone does not guarantee a successful purchase. A poorly placed gate, unclear tolerance, or untested resin can create expensive rework after the mold is finished.
The scale of the industry makes disciplined sourcing essential. PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of plastics production worldwide in 2023. The 2024 UNCTAD Review of Maritime Transport also notes that shipping carries over 80% of global merchandise trade by volume. Your mold may be built in one country, molded in another, and shipped across several ports. Every handoff matters.
This guide presents seven practical tips for buyers evaluating Rapid Injection Molding suppliers. They cover design-for-manufacturing reviews, resin selection, tooling ownership, realistic tolerances, sample approval, quality documentation, and landed-cost planning. Ask for measurable evidence, not polished promises. Request material certificates, first-article inspection results, dimensional reports, and photographs of critical features.
Small details matter.
A supplier may quote a ten-day mold, yet exclude testing, packaging, or ocean delays. That is not necessarily dishonest, but it is incomplete. Buyers should challenge assumptions before approving production. Even experienced teams sometimes overvalue speed and undervalue repeatability. The better decision balances cycle time, part quality, compliance, logistics, and total cost. These tips are designed to support that balance across international sourcing projects.
Define Project Requirements and Global Sourcing Goals
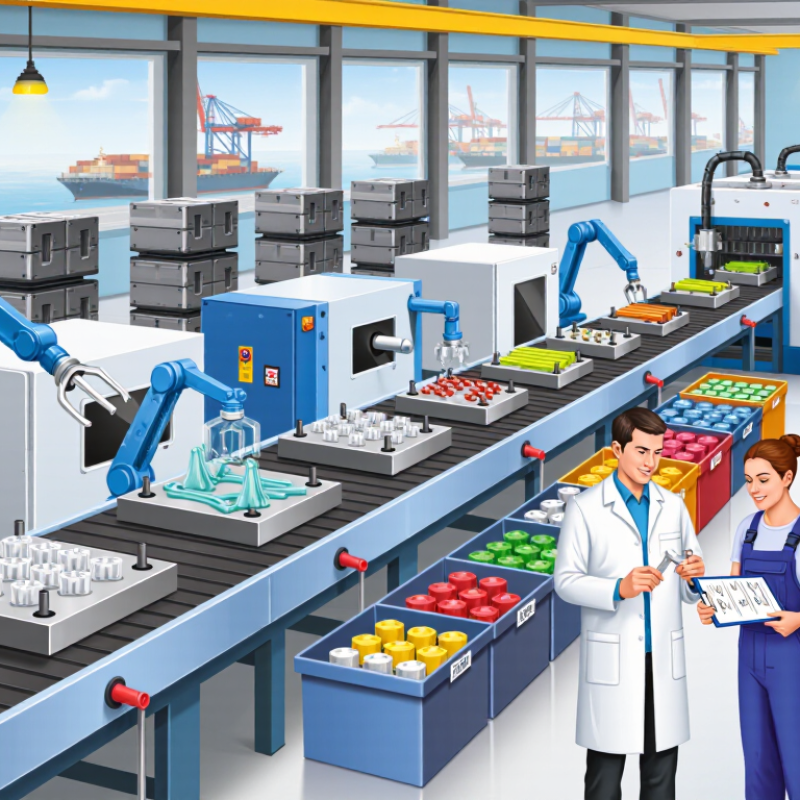
Global injection molding projects rarely fail because of molding alone. They fail when requirements remain vague across borders. Define the part’s function, dimensions, material, surface finish, expected volume, and delivery date. Add measurable tolerances, not phrases such as “high quality.” A simple drawing with redlined critical areas can prevent expensive assumptions. State whether the mold supports prototypes, pilot runs, or long-term production.
Your sourcing goal should be equally specific. Is the priority lower landed cost, faster launch, regional backup, or stable volume pricing? Calculate more than the quoted unit price. Include tooling, packaging, freight, duties, inspection, maintenance, and possible design changes. Ask potential suppliers how they control resin drying, mold temperature, flash, warpage, and first-article approval. Request process records and sample parts where practical. An experienced supplier should explain risks without hiding behind optimistic dates.
In real sourcing projects, teams sometimes choose the lowest quotation and pay more through delays. That choice looked efficient on paper. It was not. Leave room for uncertainty. Confirm communication hours, drawing revision control, tooling ownership, and corrective-action timing. Define acceptance criteria before production begins. Still, no plan is perfect. A late material change or overlooked undercut can disrupt the schedule. Review the design with manufacturing specialists before approving the mold.
7 Rapid Injection Molding Tips for Global Buyers? - Define Project Requirements and Global Sourcing Goals
| Rapid Tip | Project Requirement to Define | Global Sourcing Goal | Recommended Planning Data | Supplier Evidence to Request | Key Risk Controlled |
|---|---|---|---|---|---|
| 1 Lock the part definition early | Provide a released 3D CAD file, 2D drawing, revision number, material specification, surface-finish requirements, color reference, and critical-to-function dimensions. | Ensure every shortlisted supplier quotes the same part configuration and revision. | 100% of quotation documents should reference the same drawing revision, material grade, and annual volume. | Signed drawing review, design-for-manufacturing feedback, deviation list, and quotation assumptions. | Uncontrolled revisions, inconsistent quotations, rework, and disputes over acceptance criteria. |
| 2 Separate prototype and production goals | State whether the immediate objective is design validation, functional testing, pilot production, or full-rate manufacturing. | Select tooling and process methods that match the required quantity, speed, and expected tool life. | Define prototype quantity, launch quantity, annual demand, target tool life, and required production start date. | Tooling concept, cavity count, estimated cycle time, sample plan, and production-capacity statement. | Paying for production-level tooling when only short-run validation is needed, or using temporary tooling for long-term demand. |
| 3 Set measurable quality criteria | Identify critical dimensions, allowable cosmetic defects, flash limits, warpage expectations, assembly requirements, and inspection methods. | Create a consistent acceptance standard that can be applied regardless of supplier location. | Use a dimensional inspection plan with nominal values, tolerances, sample size, measurement equipment, and approved defect photographs where applicable. | Control plan, first-article inspection report, capability data for critical dimensions, and calibration records. | Subjective inspections, inconsistent measurements, hidden quality costs, and rejected shipments. |
| 4 Specify the material completely | Define polymer family, grade requirements, reinforcement, flame rating, color, regulatory requirements, recycled-content limits, and approved substitutions. | Prevent unauthorized material changes and maintain comparable part performance across regions. | Record resin grade, supplier documentation requirements, lot traceability, drying conditions, and material test requirements. | Technical data sheet, safety data sheet, certificate of analysis, incoming-material records, and retained sample policy. | Dimensional variation, reduced strength, appearance defects, regulatory nonconformance, and inconsistent processing. |
| 5 Compare landed cost, not unit price only | Request a cost breakdown covering tooling, parts, packaging, inspection, freight, duties, taxes, payment terms, and possible engineering charges. | Compare suppliers using the total delivered cost to the destination market. | Calculate landed cost per part using the same quantity, delivery term, transport mode, currency basis, and packaging assumptions. | Itemized quotation, tooling ownership terms, packaging specification, delivery-term definition, and validity period. | Low quoted unit price being offset by freight, import charges, tooling fees, expedited shipping, or change-order costs. |
| 6 Build a realistic global timeline | Map design approval, mold design, tool fabrication, first trial, sample approval, production ramp-up, freight, customs, and buffer time. | Achieve the required market-launch date with visible schedule ownership and contingency planning. | Track milestone dates, responsible parties, transit duration, customs lead time, and a documented schedule buffer. | Detailed project schedule, weekly status reports, trial-shot plan, corrective-action timing, and logistics plan. | Missed launches caused by unplanned tooling iterations, holidays, port delays, customs holds, or slow approvals. |
| 7 Protect continuity and ownership | Define mold ownership, storage location, maintenance responsibility, spare-part access, confidentiality, approved suppliers, and exit procedures. | Reduce dependence on one source and preserve the ability to transfer production if quality, capacity, or logistics conditions change. | Establish a documented backup plan, critical spare-parts list, maintenance intervals, and a tool-transfer process. | Tooling agreement, maintenance records, business-continuity plan, capacity information, and corrective-action history. | Production interruption, loss of tooling control, confidential-design exposure, and costly supplier transitions. |